Engineering · Reference
Thread spec library.
UNC, UNF, metric coarse, metric fine, NPT pipe, BSP parallel — with major diameter and recommended tap drill for each thread. Clean, table-first reference for engineers reviewing prints and machinists at the toolbox.
01
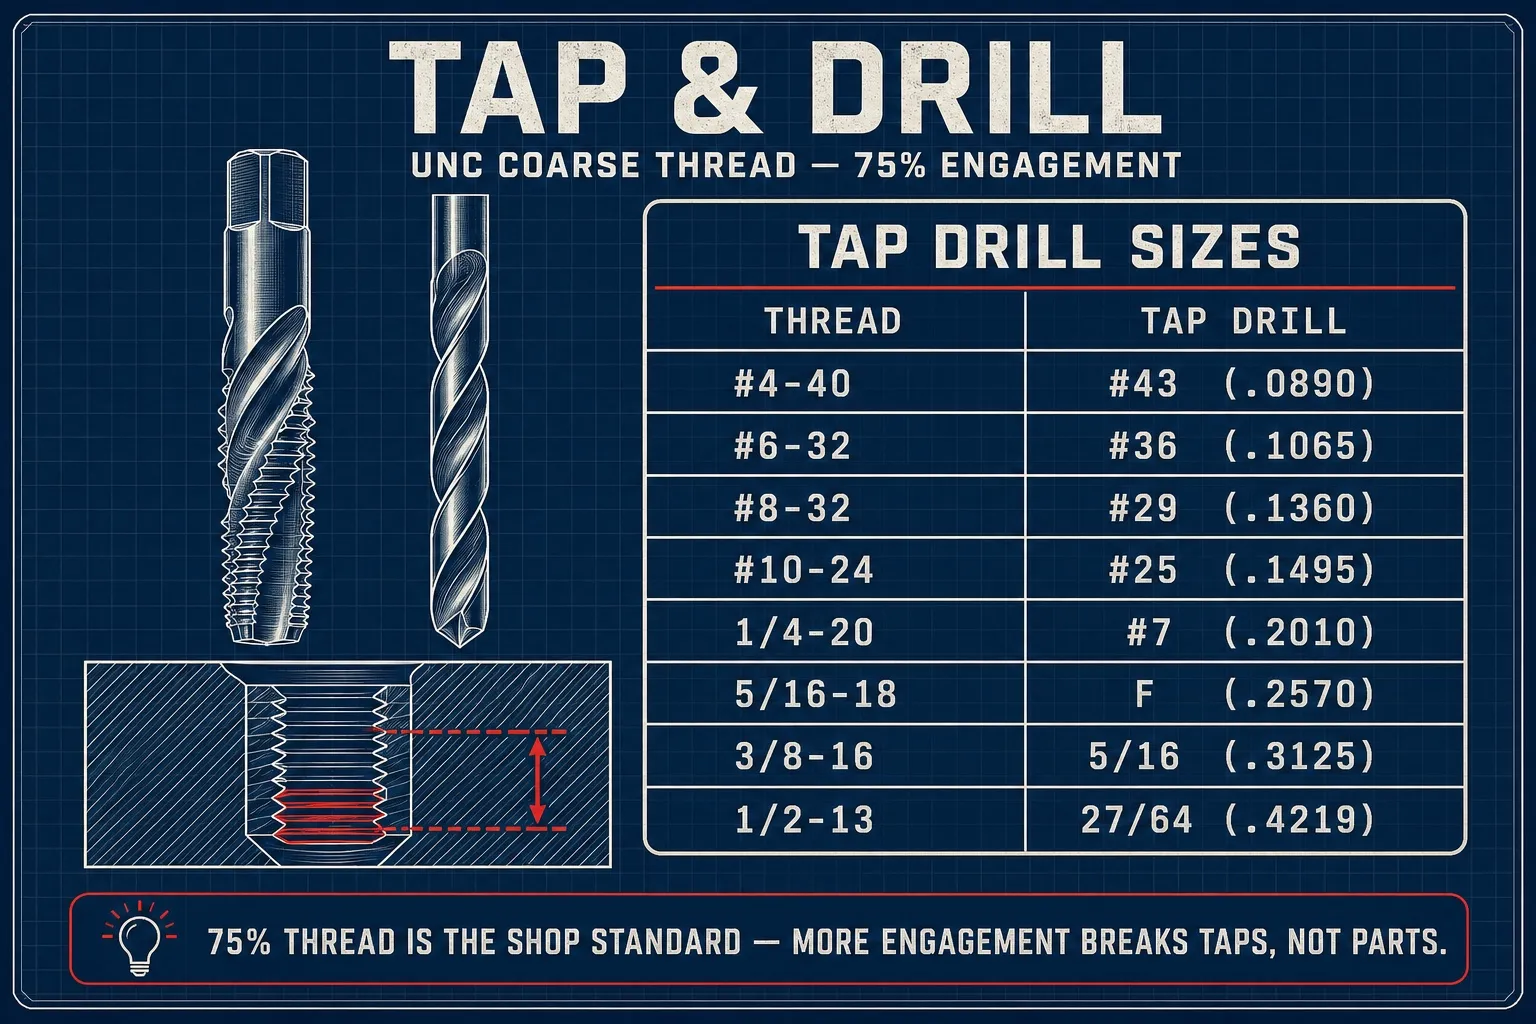
UNC — Unified National Coarse
18 sizes
| Designation | Pitch | Major dia (in) | Tap drill |
|---|---|---|---|
| #1-64 | 64 | 0.0730 | #53 (0.0595) |
| #2-56 | 56 | 0.0860 | #50 (0.0700) |
| #4-40 | 40 | 0.1120 | #43 (0.0890) |
| #5-40 | 40 | 0.1250 | #38 (0.1015) |
| #6-32 | 32 | 0.1380 | #36 (0.1065) |
| #8-32 | 32 | 0.1640 | #29 (0.1360) |
| #10-24 | 24 | 0.1900 | #25 (0.1495) |
| #12-24 | 24 | 0.2160 | #16 (0.1770) |
| 1/4-20 | 20 | 0.2500 | #7 (0.2010) |
| 5/16-18 | 18 | 0.3125 | F (0.2570) |
| 3/8-16 | 16 | 0.3750 | 5/16 (0.3125) |
| 7/16-14 | 14 | 0.4375 | U (0.3680) |
| 1/2-13 | 13 | 0.5000 | 27/64 (0.4219) |
| 9/16-12 | 12 | 0.5625 | 31/64 (0.4844) |
| 5/8-11 | 11 | 0.6250 | 17/32 (0.5313) |
| 3/4-10 | 10 | 0.7500 | 21/32 (0.6563) |
| 7/8-9 | 9 | 0.8750 | 49/64 (0.7656) |
| 1-8 | 8 | 1.0000 | 7/8 (0.8750) |
02
UNF — Unified National Fine
19 sizes
| Designation | Pitch | Major dia (in) | Tap drill |
|---|---|---|---|
| #0-80 | 80 TPI | 0.0600 | 3/64 (0.0469) |
| #1-72 | 72 | 0.0730 | #53 (0.0595) |
| #2-64 | 64 | 0.0860 | #50 (0.0700) |
| #3-56 | 56 | 0.0990 | #45 (0.0820) |
| #4-48 | 48 | 0.1120 | #42 (0.0935) |
| #5-44 | 44 | 0.1250 | #37 (0.1040) |
| #6-40 | 40 | 0.1380 | #33 (0.1130) |
| #8-36 | 36 | 0.1640 | #29 (0.1360) |
| #10-32 | 32 | 0.1900 | #21 (0.1590) |
| 1/4-28 | 28 | 0.2500 | #3 (0.2130) |
| 5/16-24 | 24 | 0.3125 | I (0.2720) |
| 3/8-24 | 24 | 0.3750 | Q (0.3320) |
| 7/16-20 | 20 | 0.4375 | 25/64 (0.3906) |
| 1/2-20 | 20 | 0.5000 | 29/64 (0.4531) |
| 9/16-18 | 18 | 0.5625 | 33/64 (0.5156) |
| 5/8-18 | 18 | 0.6250 | 37/64 (0.5781) |
| 3/4-16 | 16 | 0.7500 | 11/16 (0.6875) |
| 7/8-14 | 14 | 0.8750 | 13/16 (0.8125) |
| 1-12 | 12 | 1.0000 | 59/64 (0.9219) |
03
Metric — Coarse (ISO standard)
14 sizes
| Designation | Pitch | Major dia (mm/in) | Tap drill |
|---|---|---|---|
| M1.6 × 0.35 | 0.35 mm | 1.60 (0.0630) | 1.25 mm (0.0492) |
| M2 × 0.4 | 0.40 | 2.00 (0.0787) | 1.6 mm (0.0630) |
| M2.5 × 0.45 | 0.45 | 2.50 (0.0984) | 2.05 mm (0.0807) |
| M3 × 0.5 | 0.50 | 3.00 (0.1181) | 2.5 mm (0.0984) |
| M4 × 0.7 | 0.70 | 4.00 (0.1575) | 3.3 mm (0.1299) |
| M5 × 0.8 | 0.80 | 5.00 (0.1969) | 4.2 mm (0.1654) |
| M6 × 1.0 | 1.00 | 6.00 (0.2362) | 5.0 mm (0.1969) |
| M8 × 1.25 | 1.25 | 8.00 (0.3150) | 6.8 mm (0.2677) |
| M10 × 1.5 | 1.50 | 10.00 (0.3937) | 8.5 mm (0.3346) |
| M12 × 1.75 | 1.75 | 12.00 (0.4724) | 10.2 mm (0.4016) |
| M14 × 2.0 | 2.00 | 14.00 (0.5512) | 12.0 mm (0.4724) |
| M16 × 2.0 | 2.00 | 16.00 (0.6299) | 14.0 mm (0.5512) |
| M20 × 2.5 | 2.50 | 20.00 (0.7874) | 17.5 mm (0.6890) |
| M24 × 3.0 | 3.00 | 24.00 (0.9449) | 21.0 mm (0.8268) |
04
Metric — Fine
10 sizes
| Designation | Pitch | Major dia (mm/in) | Tap drill |
|---|---|---|---|
| M3 × 0.35 | 0.35 mm | 3.00 (0.1181) | 2.65 mm (0.1043) |
| M4 × 0.5 | 0.50 | 4.00 (0.1575) | 3.5 mm (0.1378) |
| M5 × 0.5 | 0.50 | 5.00 (0.1969) | 4.5 mm (0.1772) |
| M6 × 0.75 | 0.75 | 6.00 (0.2362) | 5.25 mm (0.2067) |
| M8 × 1.0 | 1.00 | 8.00 (0.3150) | 7.0 mm (0.2756) |
| M10 × 1.25 | 1.25 | 10.00 (0.3937) | 8.8 mm (0.3465) |
| M12 × 1.5 | 1.50 | 12.00 (0.4724) | 10.5 mm (0.4134) |
| M14 × 1.5 | 1.50 | 14.00 (0.5512) | 12.5 mm (0.4921) |
| M16 × 1.5 | 1.50 | 16.00 (0.6299) | 14.5 mm (0.5709) |
| M20 × 1.5 | 1.50 | 20.00 (0.7874) | 18.5 mm (0.7283) |
05
NPT — National Pipe Thread (tapered)
7 sizes
| Designation | Pitch | Major dia (in) | Tap drill | Notes |
|---|---|---|---|---|
| 1/16-27 | 27 TPI | 0.3125 | C (0.2420) | Tapered 1°47′ |
| 1/8-27 | 27 | 0.4050 | R (0.3390) | Tapered 1°47′ |
| 1/4-18 | 18 | 0.5400 | 7/16 (0.4375) | Tapered 1°47′ |
| 3/8-18 | 18 | 0.6750 | 37/64 (0.5781) | Tapered 1°47′ |
| 1/2-14 | 14 | 0.8400 | 23/32 (0.7188) | Tapered 1°47′ |
| 3/4-14 | 14 | 1.0500 | 59/64 (0.9219) | Tapered 1°47′ |
| 1-11.5 | 11.5 | 1.3150 | 1-5/32 (1.1563) | Tapered 1°47′ |
06
BSP — British Standard Pipe (parallel)
6 sizes
| Designation | Pitch | Major dia | Tap drill |
|---|---|---|---|
| G1/8 (28 TPI) | 28 | 9.728 mm | 8.7 mm |
| G1/4 (19 TPI) | 19 | 13.157 mm | 11.7 mm |
| G3/8 (19 TPI) | 19 | 16.662 mm | 15.2 mm |
| G1/2 (14 TPI) | 14 | 20.955 mm | 19.0 mm |
| G3/4 (14 TPI) | 14 | 26.441 mm | 24.2 mm |
| G1 (11 TPI) | 11 | 33.249 mm | 30.5 mm |
07
Helicoil — STI tap-drill rule
Helicoil (and equivalent wire-thread inserts) require an oversize pre-drill: the STI (Screw Thread Insert) tap cuts a thread large enough to hold the coil, so the drill ends up slightly larger than the screw’s nominal (major) diameter. Size it from the STI tap chart (ASME B18.29.1 for inch), which is keyed to the nominal diameter — not by adding an offset to the standard tap drill.
- Inch: STI drill ≈ nominal (major) diameter + ~0.008–0.016″ from #4 through 1/2″ — e.g. #10-24 = 13/64, 1/4-20 = 17/64 (0.2656″), 3/8-16 = 25/64, 1/2-13 = 33/64. Larger sizes run more (5/8-11 = 21/32).
- Metric: STI drill ≈ nominal (major) diameter + ~0.2–0.5 mm, depending on thread size — e.g. M6×1 = 6.3 mm.
- Always check the manufacturer’s STI chart for the specific insert series — Heli-Coil, Recoil, and Time-Sert have small differences.
- Tap with an STI tap, not a standard tap. STI taps are oversize to match the pre-drill.
When to specify which
Picking the right thread series.
- UNC for general assembly + soft material.
Coarse pitch tolerates rougher manufacturing and resists stripping in aluminum, cast iron, or plastic. Default for most non-critical structural fasteners.
- UNF for vibration + hard material.
Fine pitch resists loosening from vibration, gives finer torque control. Standard for aerospace structural fasteners and steel-on-steel.
- Metric coarse for international + ISO drawings.
Default international standard. M6, M8, M10 are the workhorses.
- Metric fine for precision + thin wall.
Better engagement on thin sections and finer pitch for fine-adjustment applications.
- NPT for tapered pipe sealing.
Tapered thread (1°47′ angle) seals by interference. Standard for North American hydraulic and pneumatic plumbing; usually paired with thread sealant.
- BSP for European pipe + fluid power.
G-series is parallel; R-series is tapered. Common on European hydraulic equipment. Not interchangeable with NPT.
For tap-drill recommendations and depth/torque calculations, see the tap-drill calculator and bolt-torque calculator.
Keep exploring
Related tools & references
Drill size for any thread at a chosen percent of thread engagement.
Number, letter, fractional, and metric drill decimal equivalents.
Through-hole sizes for bolt and screw pass-through fits.
Head recess dimensions for flat- and socket-head fasteners.
Minimum engagement length for full fastener strength.
Target torque from thread size, grade, and lubrication.
Have a part that needs to be made right?
Tell us about your part and we'll get back to you promptly. Aerospace, medical, defense, and semiconductor production work welcome.Email CAD models and drawings to sales@digitalmachine.com, including ITAR, EAR, CUI and AS9100 work. Keep controlled technical data out of web forms.
First articles through full production runs